Precision-engineered 12V / 24V BLDC inline pressure boosters customized for smart toilets, bidets, sanitary ware, and compact fluid circulation.
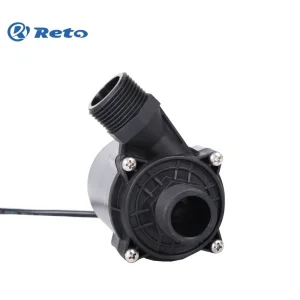
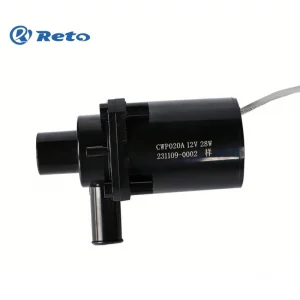
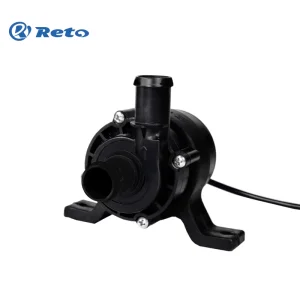
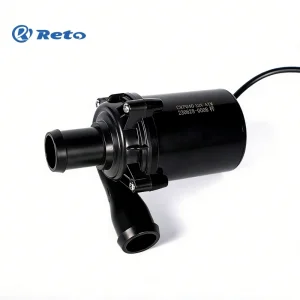
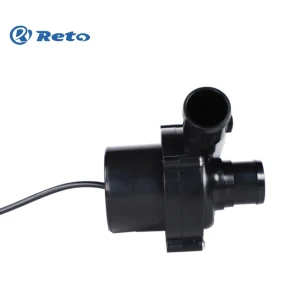
Re-architecting pressure boosting through magnetic coupling, sensorless vector control, and ultra-durable materials.
In modern hydraulic engineering, the term inline water pressure pump refers to an axially oriented pumping mechanism integrated directly within a fluid conduit line without requiring significant piping re-routing. Unlike conventional bulky centrifugal surface pumps or traditional AC-driven booster systems, modern inline pressure pumps—specifically those leveraging Brushless DC (BLDC) technology—have revolutionized municipal, residential, and industrial OEM application landscapes.
Global original equipment manufacturers (OEMs) across smart sanitary engineering, electric vehicle (EV) thermal regulation, instant water heating, micro-grid solar hydraulics, and commercial water purification face increasing pressures to shrink hardware footprints while enhancing energy conversion ratios, operating life, and acoustic comfort. As a nationally certified high-tech enterprise, Xiamen Reto Electric Appliances Co., Ltd. (RETO) stands at the forefront of this industrial transition, holding over 50 patents and maintaining ISO9001 and automotive-grade IATF16949 quality standard certifications.
Traditional inline pressure boosters relied heavily on brushed AC induction motors or basic brushed DC configurations. These legacy designs suffer from significant structural limitations: mechanical shaft seals prone to wear and seal friction leaks, carbon brush degradation resulting in electromagnetic interference (EMI) and localized sparking, high thermal output, and elevated operational noise levels often exceeding 55 to 60 dB(A).
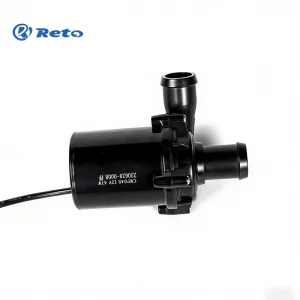
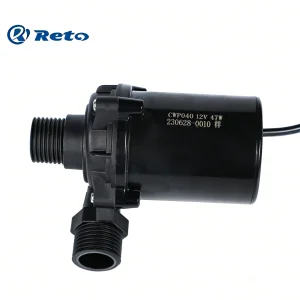
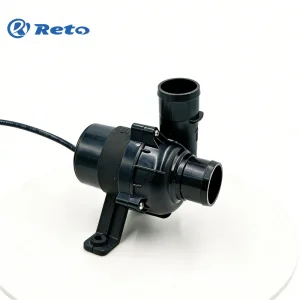
To overcome these challenges, RETO's advanced inline water pressure pumps incorporate a static seal, magnetic drive coupling architecture. The motor stator drives a ceramic-shaft-mounted permanent magnet rotor encapsulated entirely within a hermetically sealed fluid chamber. Key engineering parameters include:
By shifting from mechanical seals to magnetic drive BLDC architecture, total system efficiency increases by up to 35% while eliminating fluid leakage risks. Modern BLDC inline pressure pumps consume up to 45% less standby and operational electrical energy compared to traditional AC shaded-pole booster pumps.
Macro drivers reshaping the global fluid pump supply chain through 2030.
The global surge in off-grid residential installations and solar thermal water heating systems has created massive demand for low-voltage direct current (12V/24V/48V DC) inline boosters. Modern factories are rapidly phasing out high-voltage AC units in favor of safe, low-voltage DC pumps capable of direct integration with solar PV micro-controllers and battery storage banks.
Smart toilets and bidets require extreme physical compacting without compromising hydraulic head pressure. Contemporary smart toilets mandate pressure boosting capable of delivering rapid impulse flushing (up to 20–30 L/min instantaneous flow) while maintaining noise envelopes below 38 dB(A) for residential master suite comfort.
Next-generation industrial chillers, commercial water purifiers, and home heating manifolds are embedding microcontrollers into inline pumps. Features such as dry-run protection, stall detection, locked-rotor auto-recovery, and real-time operational feedback via LIN/CAN bus or PWM frequency signals are now baseline requirements for global Tier-1 OEMs.
Evaluating technical criteria, factory audit protocols, and material compliance for contract manufacturing.
Procurement directors and hydraulic design engineers from Fortune 500 enterprises evaluate custom inline water pressure pump suppliers based on a strict matrix of manufacturing maturity, quality assurance controls, and material compliance. Selecting an OEM partner requires looking beyond unit price to evaluate the total cost of quality (CoQ) over the product's operational lifecycle.
| Evaluation Metric | Standard Commercial Supplier | RETO Enterprise OEM Standard | Impact on OEM End-Product |
|---|---|---|---|
| Motor Technology | Brushed DC or AC Shaded-Pole | Brushless DC (BLDC) Magnetic Drive | +300% lifespan; zero EMI interference; lower heat |
| Acoustic Rating | 48 dB(A) - 58 dB(A) | < 38 dB(A) @ 1 meter | Enables bedroom-adjacent installation |
| Hydraulic Housing | Standard Recycled ABS/PVC | Food-Grade PPE / PPS / 316 Stainless | Prevents chemical leaching; handles high thermal pressure |
| Quality Certification | Basic ISO9001 only | ISO9001, IATF16949, TÜV Certified | Automotive-grade process stability & tracebility |
| Testing Protocol | Batch Sampling (AQL 1.0) | 100% End-of-Line (EOL) Automated Testing | Near-zero defective PPM rate upon factory arrival |
Tailored inline pressure boosting configurations engineered for specialized sectoral challenges.
Engineered to deliver high instantaneous flow rates (up to 25 L/min) to overcome low municipal line pressures. Features dual-stage pressure boosting, rapid startup response times (<100ms), and thermal insulation for integrated hot water spray modules.
Built with high-temperature resistant polyphenylene sulfide (PPS) pump chambers capable of continuously handling water temperatures up to 100°C. Delivers stable inline pressure to prevent cold-water backflow spikes during shower mixing.
Designed under strict automotive IATF16949 guidelines to circulate glycol coolant mixtures across battery banks and inverter modules. Features wide ambient operating temperature ranges (-40°C to 105°C) and robust vibration resistance.
Ensuring seamless market access across North America, Europe, Asia-Pacific, and emerging markets.
Expanding into international markets requires navigating a complex matrix of regional electrical, chemical, and sanitary safety standards. RETO provides end-to-end compliance support, ensuring that custom inline water pressure pump assemblies arrive pre-certified for target destination markets.
Our custom pumps comply with UL electrical safety metrics, FCC Class B electromagnetic radiation standards, and California Proposition 65 drinking water safety directives. Components in contact with potable water utilize certified lead-free NSF/ANSI 61 compliant polymers.
All production series carry CE marking, TÜV certification, RoHS heavy metal restrictions, and REACH chemical safety registration. For sanitary and heating installations across Europe, components meet WRAS (UK) and KTW/W270 (Germany) hygiene benchmarks.
RETO offers worldwide OEM partners dedicated engineering support, including 3D CAD modeling, custom hydraulic head/flow curve adjustments, customized wire harness connectors, and fast-track 7-day rapid prototype samples.
Pioneering the future of intelligent, whisper-quiet, and energy-neutral inline pressure pumps.
As smart home ecosystems and green industrial energy standards mature, RETO's engineering team is actively advancing three core technological pillars within our micro-pump R&D laboratories:
Utilizing computational fluid dynamics (CFD) optimization to redesign internal volutes and impellers, combined with magnetic levitation ceramic thrust bearings to virtually eliminate mechanical vibration and liquid turbulence noise.
Embedding micro-pressure sensors and temperature probes directly into the internal pump housing, allowing autonomous pressure boosting control without requiring external pressure switches or external sensing plumbing.
Pioneering the use of bio-based engineering plastics and rare-earth-minimized permanent magnet rotors to lower carbon footprints across the full product lifecycle while increasing thermal deformation thresholds.
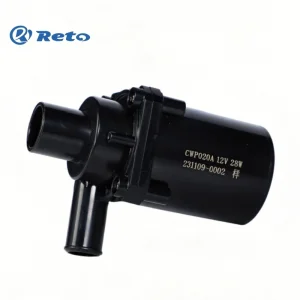
Specialized industrial, solar thermal, external pressure boosting, and energy-saving BLDC pump models.
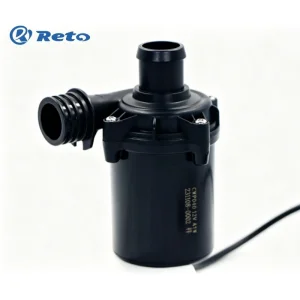
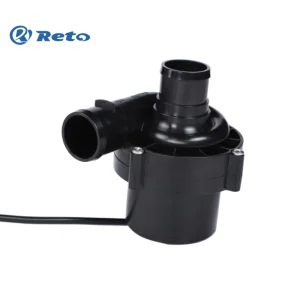
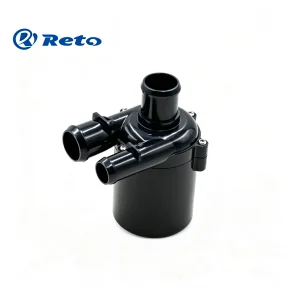
Addressing critical technical, procurement, and integration inquiries for hardware engineers and supply chain leaders.